THAILAND · INTEGRATED RO MONITORING
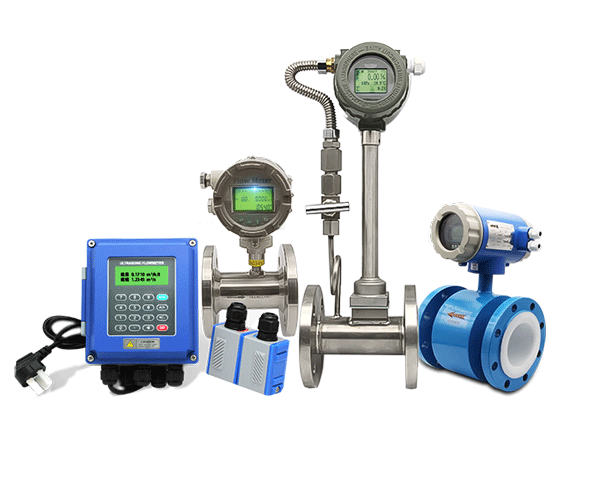
GMF100 + GWQ-MP200 + GPT200 + GLT500
Complete Monitoring Solution for RO Water Treatment
Flow + Water Quality + Pressure + Level — Four essential measurements in one integrated system | Protect RO membranes, optimize energy consumption, ensure water quality compliance
Request Quote
RO Water Treatment in Thailand
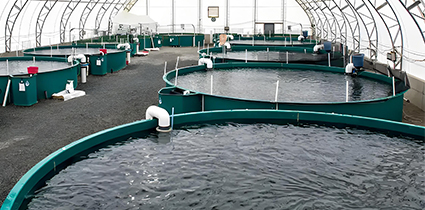
Thailand's industrial and municipal water sectors are increasingly adopting reverse osmosis (RO) technology to address water scarcity, stringent discharge regulations, and the need for high-purity process water. From electronics manufacturing in the Eastern Economic Corridor (EEC) to food & beverage plants and municipal desalination in coastal provinces, RO systems are critical infrastructure. However, RO membranes are sensitive to fouling, scaling, and oxidation—requiring precise monitoring of flow, water quality, pressure, and tank levels to maintain performance and extend membrane life.
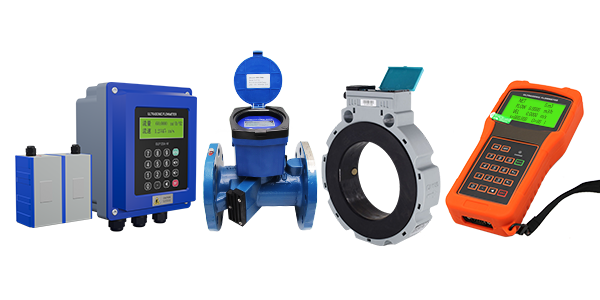
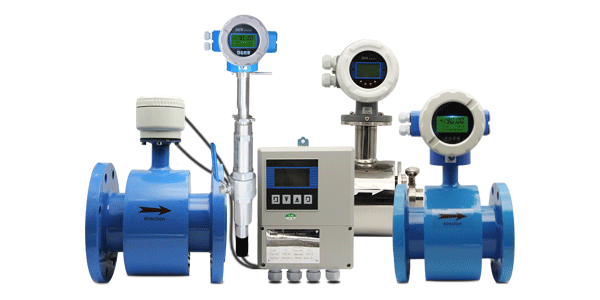
Integrated Solution: Four GAIMC Products
-
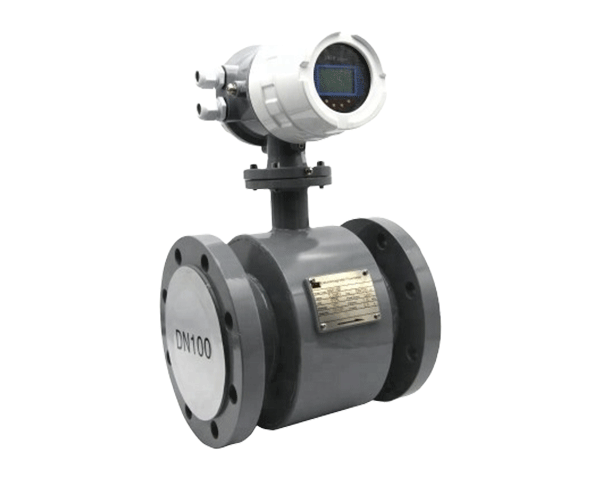
GMF100: Electromagnetic flow meter — ±0.5%, DN10–DN2200, RS485
-
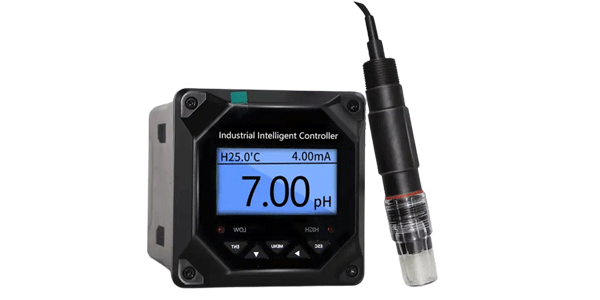
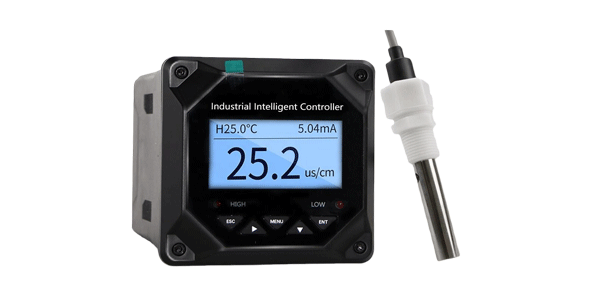
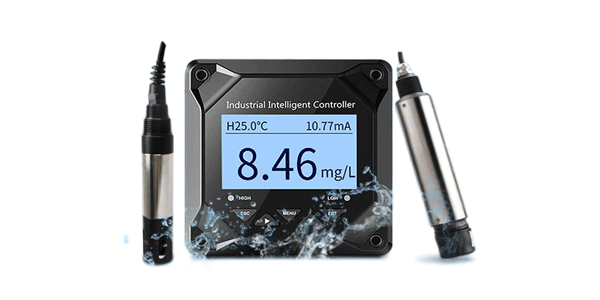
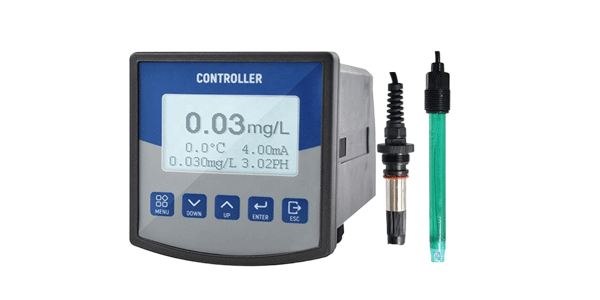
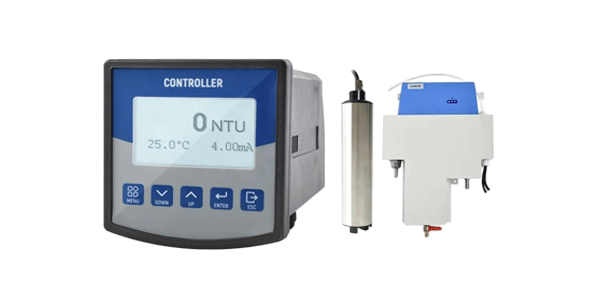
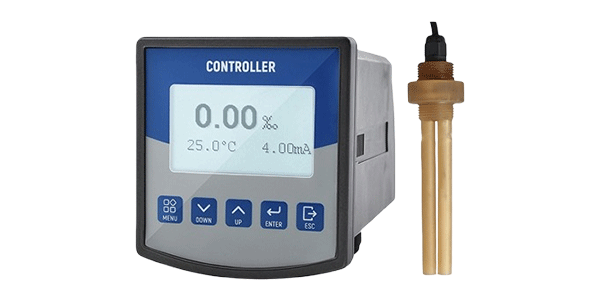
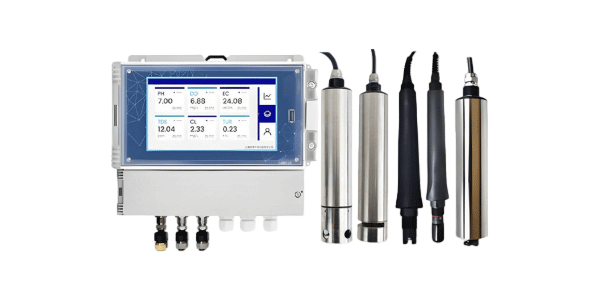
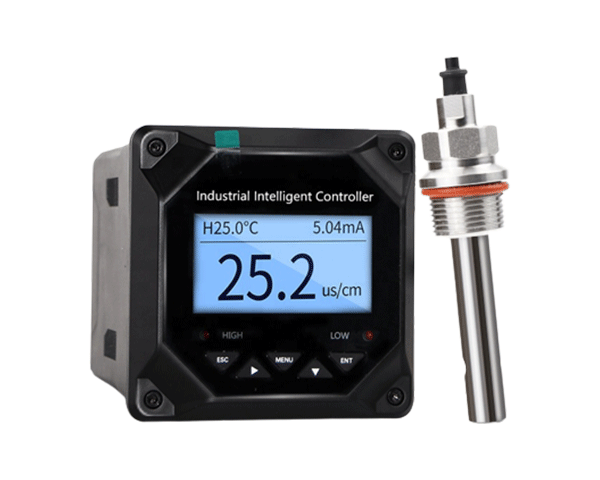
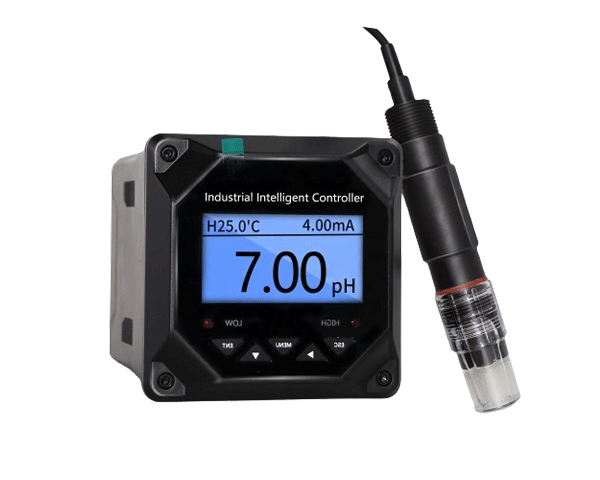
GWQ-MP200: Multi-parameter analyzer — pH, EC, ORP, chlorine, turbidity
-
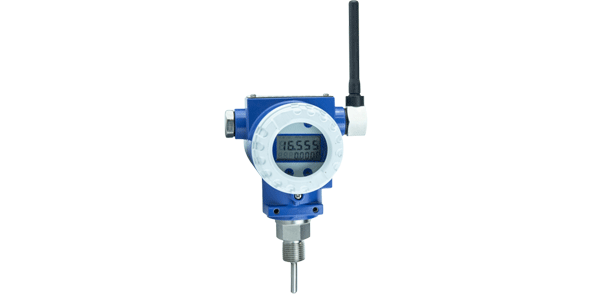
GPT200: Pressure transmitter — 0.1% accuracy, 316L SS, multiple outputs
-
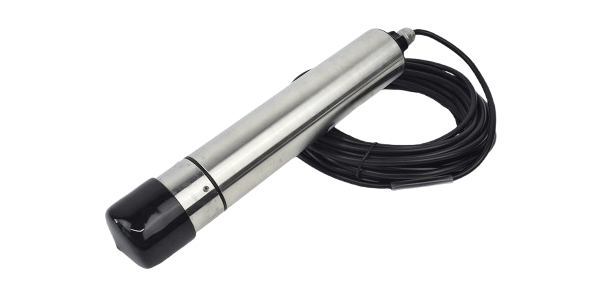
GLT500: Level transmitter — submersible, IP68, 0~200mH₂O
Top 4 RO Water Treatment Pain Points in Thailand
Challenges impacting membrane life, energy costs, and water quality
Membrane Scaling & Fouling
Inadequate monitoring of pH, conductivity, and pressure leads to scaling and fouling, reducing permeate flow and increasing energy costs.
Flow Imbalance & Energy Waste
Without accurate flow measurement on feed, permeate, and concentrate lines, pump efficiency and recovery rates cannot be optimized.
Pressure & Level Blind Spots
High-pressure pump protection and tank level monitoring are critical for preventing equipment damage and ensuring continuous supply.
Disconnected Data Systems
Separate instruments for flow, quality, pressure, and level create data silos, making unified process control difficult.
Integrated RO Monitoring Solution
Four GAIMC products covering flow, water quality, pressure, and level
GMF100 Electromagnetic Flow Meter
GMF100 — ±0.5% accuracy, DN10~DN2200
|
Specification
|
Details
|
|
Diameter range
|
DN10–DN2200 mm
|
|
Accuracy
|
±0.5%
|
|
Flow rate
|
0.3–10 m/s
|
|
Communication
|
RS485 (Modbus-RTU), GPRS, HART
|
|
Power supply
|
220VAC / 24VDC / lithium battery
|
|
Protection
|
IP65/IP67/IP68
|
✔ Suitable for raw water, RO feed, permeate, and concentrate lines
GWQ-MP200 Multi-Parameter Analyzer
GWQ-MP200 — 1~6 channels, RTOS, touchscreen
|
Specification
|
Details
|
|
Parameters
|
pH, ORP, EC, TDS, DO, chlorine, turbidity, etc.
|
|
Channels
|
1 to 6
|
|
Communication
|
2x RS485 (Modbus-RTU)
|
|
Output
|
2x isolated 4-20mA
|
|
Relays
|
6 relays
|
|
Data storage
|
8GB TF card (max 32GB)
|
✔ Monitors RO feed water quality and permeate purity
GPT200 Universal Pressure Transmitter
GPT200 — 0.1% accuracy, 316L SS diaphragm
|
Specification
|
Details
|
|
Pressure range
|
-0.1MPa...0kPa~10kPa...100MPa
|
|
Accuracy
|
0.1%, 0.25%, 0.5% FS
|
|
Output
|
4-20mA, 0-5V, 0-10V, 0.5-4.5V
|
|
Diaphragm
|
316L SS or Titanium
|
|
Protection
|
IP65 (IP68 customizable)
|
|
Response time
|
≤1 ms
|
✔ High-pressure pump protection and differential pressure monitoring
GLT500 Level Transmitter
GLT500 — Submersible, IP68, 0~200mH₂O
|
Specification
|
Details
|
|
Pressure range
|
0~1m...200mH₂O
|
|
Accuracy
|
±0.25%FS, ±0.5%FS
|
|
Output
|
4-20mA, 0-5V, 1-5V, RS485
|
|
Protection
|
IP68
|
|
Certification
|
Explosion-proof, CE
|
|
Medium
|
Compatible with 316L SS
|
✔ Raw water tank, permeate storage, and concentrate sump level monitoring
Integrated RO Plant Monitoring Architecture
System Components & Installation Points:
-
GLT500 — Raw water tank & permeate storage tank level
-
GPT200 — High-pressure pump inlet/outlet pressure & membrane differential pressure
-
GWQ-MP200 — RO feed pH, conductivity, ORP, and residual chlorine
-
GMF100 — Feed, permeate, and concentrate flow measurement
-
All devices communicate via RS485 (Modbus-RTU) to central PLC/SCADA
Key Integration Benefits:
-
Complete process visibility from intake to permeate storage
-
Early warning for membrane scaling, fouling, and oxidation
-
Optimized energy consumption through pressure and flow control
-
Historical data logging for compliance and maintenance planning
Integrated RO Monitoring Deployments
Real installations: industrial RO plants, water reuse facilities, and municipal desalination
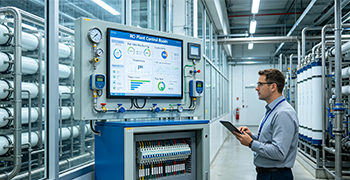
📊 Integrated monitoring system in RO plant control room
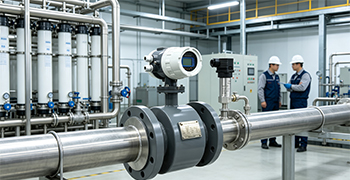
🔧 GMF100 flow meter on RO feed line + GPT200 pressure transmitter
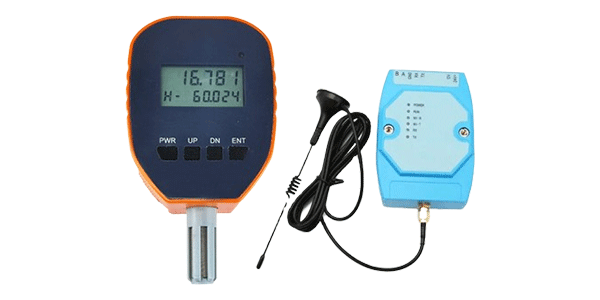
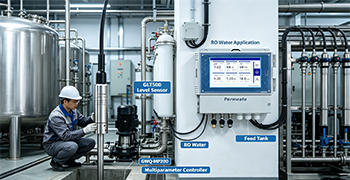
📱 GWQ-MP200 Water quality+GLT500 Level sensor
Based on deployments in Thai industrial estates and water treatment facilities — contact us for detailed case photos
Real Case: Industrial RO Plant (Rayong, Thailand)
Challenge: Membrane fouling and high energy costs in a 2,000 m³/day RO facility
Facility Background
A 2,000 m³/day industrial RO plant in Rayong Province supplies high-purity process water to an electronics manufacturing facility in the Eastern Economic Corridor (EEC). The plant was experiencing frequent membrane cleaning cycles (every 6–8 weeks) and higher-than-expected energy consumption due to fouling and suboptimal operating pressures. Differential pressure across the membrane array was not continuously monitored, and permeate flow was only checked manually once per shift.
Integrated GAIMC Implementation
Deployed a complete monitoring system: GMF100 electromagnetic flow meters on feed, permeate, and concentrate lines; GWQ-MP200 with pH, conductivity, ORP, and residual chlorine sensors on RO feed; GPT200 pressure transmitters on high-pressure pump inlet/outlet and membrane differential pressure; and GLT500 submersible level transmitters in raw water and permeate storage tanks. All devices integrated via RS485 (Modbus-RTU) to the plant's SCADA system.
Results after 6 months
50%
Reduction in membrane cleaning frequency
12%
Energy consumption reduction
99.5%
Water quality compliance maintained
“The integrated GAIMC system gave us complete visibility into our RO process. We can now detect fouling trends early, optimize pump pressures, and plan maintenance proactively. Membrane life has been extended significantly.”
— Plant Manager, Industrial RO Facility, Rayong
Key Metrics Improvement
✅ Membrane cleaning: from every 6–8 weeks → every 12–16 weeks
✅ Energy consumption: reduced by 12% through pressure optimization
✅ Real-time monitoring of 12+ critical process points
Financial Impact
Total investment recovered in 8 months through reduced cleaning chemicals, lower energy costs, and extended membrane life. The plant now serves as a model for other industrial RO facilities in Thailand's EEC.
Why GAIMC's Integrated Solution for RO?
Complete measurement coverage — Flow, water quality, pressure, and level from a single supplier, ensuring compatibility and simplified integration.
Automated process control — GWQ-MP200 relays can trigger chemical dosing and alarm systems based on real-time water quality.
Unified communication — All devices support RS485 (Modbus-RTU) for seamless SCADA/PLC integration.
Data-driven optimization — Historical logging enables trend analysis, predictive maintenance, and compliance reporting.
Combined Technical Specifications
|
Product
|
Measurement
|
Key Specs
|
|
GMF100
|
Flow
|
DN10–DN2200, ±0.5%, RS485
|
|
GWQ-MP200
|
pH, EC, ORP, chlorine, turbidity
|
1–6 channels, 2x RS485, 6 relays
|
|
GPT200
|
Pressure
|
0.1% FS, 316L SS, 4-20mA
|
|
GLT500
|
Level
|
0~200mH₂O, IP68, 4-20mA/RS485
|
※ All products support RS485 Modbus-RTU for integrated process control
Configure Your Integrated RO Monitoring System
For complete RO plant monitoring, please provide: pipe diameters, water quality parameters, pressure ranges, tank dimensions, and communication requirements. Our engineers will recommend the optimal configuration combining GMF100, GWQ-MP200, GPT200, and GLT500.